SHANGHAI, SHANGHAI, CHINA, October 25, 2026 /EINPresswire.com/ — It is 2:15 AM on a humid Tuesday at a mid-sized automotive components facility. The night shift plant engineer stands near the main compressor room, listening to the metallic whine of an aging rotary screw unit. Pressure gauges flicker down to 5.2 bar during peak pneumatic robotic assembly cycles, triggering automatic shutdown warnings across three automated lines. Downstream air drop points leak moisture onto precision CNC fixtures, while month-end utility statements show power costs climbing by 18%.
Procurement teams face a familiar dilemma: replace legacy units with another standard off-the-shelf air compressor or re-evaluate the core engineering behind industrial compressed air systems.
Plant managers seeking consistent reliability increasingly turn to the Top Rated Rotary Screw Compressors Factory in the Field.
Modern rotary screw compressors serve as the continuous-duty workhorse of industrial manufacturing, utilizing two meshing helical rotors to draw in, compress, and discharge air with lower vibration and continuous volumetric flow compared to reciprocating piston designs. As manufacturing facilities upgrade line efficiency, evaluating engineering differences between legacy compressors and modern designs becomes vital for long-term plant uptime.
Looking ahead to 2026, air equipment engineering emphasizes systemic durability, thermal efficiency, and precision rotor geometry. Industrial manufacturers face five common failure scenarios when procuring compressed air systems, each linked directly to mechanical design limits in traditional air compressor packages.
Tech Reason 1: Overcoming Air-End Internal Leakage with Precision Helical Rotor Profile Engineering
Procurement Failure Scenario 1: Volumetric Output Loss and Elevated Thermal Wear
Traditional rotary screw units often suffer from accelerated volumetric loss after 10,000 to 15,000 hours of continuous load. Standard rotor profiles exhibit wider clearance tolerances between male and female lobes, creating internal blow-by air recirculation. This internal leakage forces the motor to draw excess current to maintain target discharge pressures while raising internal oil injection temperatures.
The Technical Solution
Engineered rotor profile dynamics address internal air recirculation directly at the compression stage. Through advanced air-end engineering developed following the integration of Shanghai Rotorcomp in 2021, AIRERA integrates German EVO series air-ends featuring patented Rolling Profile geometry. By optimizing rotor contact lines and thermal oil injection ports, internal leakage paths are minimized. The design optimizes suction port efficiency and lowers internal pressure drops, maintaining stable volumetric output across operating pressure ranges from 5 to 15 barg. Reducing internal mechanical friction keeps operational temperatures lower, preserving lubricant viscosity and extending bearing service life.
Tech Reason 2: Eliminating Severe Power Spikes via High-Efficiency Drive Line Integration
Procurement Failure Scenario 2: High Utility Overhead and Unstable Motor Torque
Industrial compressed air accounts for a major portion of a plant’s total electrical consumption. Legacy fixed-speed compressors operate on crude load/unload cycles. During unload phases, the motor continues drawing 30% to 40% of full-load power while producing zero compressed air. Standard belt-driven units without automatic tension adjustments lose up to 6% drive efficiency due to belt slippage and heat buildup.
The Technical Solution
Integrating high-efficiency motor drive architectures addresses energy loss across variable plant demand cycles. Facilities utilizing variable speed drive (VSD) and permanent magnet VSD (PM-VSD) configurations match motor output directly to real-time air demand. For belt-driven packages like the AGSD-E integrated series, an automatic self-tensioning transmission system utilizes motor gravity and starting torque to maintain constant belt alignment. This design achieves transmission efficiency exceeding 98% over a design service life of up to 25,000 hours, eliminating manual retensioning downtime and reducing unneeded electrical draw.
Tech Reason 3: Preventing Downstream Moisture Contamination with Integrated Air Purity Packages
Procurement Failure Scenario 3: Condensate Carryover and Pneumatic Tool Corrosion
Procuring a standard compressor without matched air treatment equipment often leads to moisture carryover in distribution piping. Ambient humidity condenses inside main supply lines, causing rust, valve clogging in downstream robotics, and product contamination in sensitive applications like food processing, electronics, and pharmaceuticals.
The Technical Solution
Modern industrial air setups combine compression, drying, and filtration into unified systems. Tank-mounted units, such as the AGSD-E series, incorporate integrated air dryers and multi-stage line filters. By pairing high-performance cooling systems with TUV- and CE-compliant inline filtration, oil content in discharged air can be controlled down to 0.001 ppm. Upgraded cooling architectures deliver 20% to 30% higher thermal dissipation capacity compared to legacy configurations, preventing moisture carryover before air enters plant distribution headers.
Tech Reason 4: Reducing Unscheduled Maintenance with Heavy-Duty Component Specifications
Procurement Failure Scenario 4: Electrical Failure in Harsh Operating Environments
Standard off-the-shelf compressors often utilize lower-cost electrical contactors, lightweight cabinet frames, and budget control boards. When installed in ambient environments with ambient heat, dust, or continuous vibration-such as mining, petrochemical plants, or outdoor drilling sites-these components experience premature coil burnouts and control system lockouts.
The Technical Solution
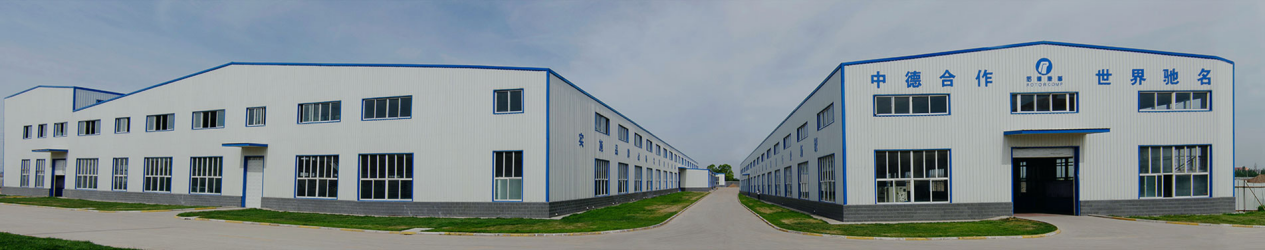
Heavy-duty component specification ensures continuous operational uptime under demanding factory conditions. Building on a manufacturing heritage established in 1999 by Shanghai Bestcomp, current production facilities across Shanghai, Hebei, and Henan utilize robust international components. Electrical cabinets integrate Schneider contactors, IP55-rated high-efficiency motors with 1.2 service factors, and intelligent color touchscreen controllers for real-time diagnostic monitoring. Supported by 106 research and development technicians and 12 third-generation patented assembly lines, these engineering standards ensure operational stability for industrial users across 53 countries.
Tech Reason 5: Eliminating System Sizing Mismatches with Modular Application-Specific Engineering
Procurement Failure Scenario 5: Single-Type Machine Deployment in Specialized Process Applications
A frequent procurement mistake involves deploying a standard oil-injected compressor into specialized applications requiring oil-free air, portable diesel power, or ultra-high pressures. Standard units struggle with nitrogen/oxygen specialty gas generation, high-pressure PET blowing, or remote site drilling, leading to premature air-end wear and severe operational inefficiencies.
The Technical Solution
Addressing diverse industrial workflows requires custom-engineered compressor platforms tailored to specific process gas and pressure needs. Global operations rely on specialized configurations including diesel portable compressors, ISO 8573-1 Class 0 oil-free screw compressors, oil-free scroll units, 2-stage screw compressors, and high-pressure air platforms. Industry leaders including Huawei, Sinopec, GE, CNNR, CNPC, BYD, TOYOTA, Air Products, and Pylontech deploy specialized air packages optimized for general manufacturing, mining, shipbuilding, semiconductor assembly, and specialty gas production.
Optimizing Factory Air Performance for 2026
Upgrading industrial air infrastructure requires moving beyond basic pressure and flow metrics to evaluate total cost of ownership, component durability, and air quality standards. For plant engineering teams reviewing 15 kW to 22 kW air requirements, integrated tank-mounted systems like the AGSD-E series offer a compact solution. Delivering 0.53 to 3.51 m3/min air volume across 8 to 15 bar operating pressures, these units combine German EVO air-end precision, quiet 69 to 71 dB(A) sound enclosure design, and low maintenance overhead into a ready-to-connect package.
To review complete mechanical specifications, CAD dimension layouts, and application guidelines for modern compressed air systems, visit https://www.aireracompressor.com/
AIRERA
AIRERA
Legal Disclaimer:
EIN Presswire provides this news content “as is” without warranty of any kind. We do not accept any responsibility or liability
for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this
article. If you have any complaints or copyright issues related to this article, kindly contact the author above.

Media gallery